High-Performance Servo & Hub Motor Assemblies
Explore our engineered motion control platforms, tailored for high torque density, rigorous duty cycles, medical-grade compliance, and micro-mobility integration.
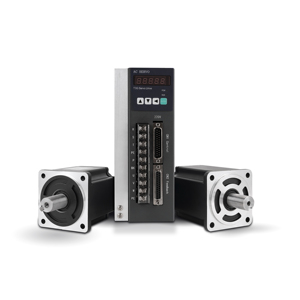
AC Servo Motor 1300W 220V Support Pulse / RS485 Control
Precision-engineered for medical equipment and high-efficiency automation. Features ultra-low cogging torque and high dynamic response.
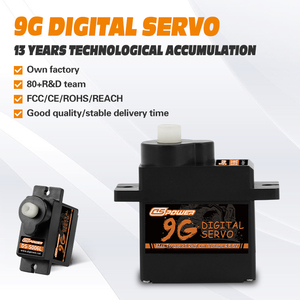
SG90 Servo Motor PWM 180° Micro Servo DSPOWER
Compact plastic/metal gear micro actuator designed for rapid positional feedback, robotic end-effectors, and lightweight control systems.
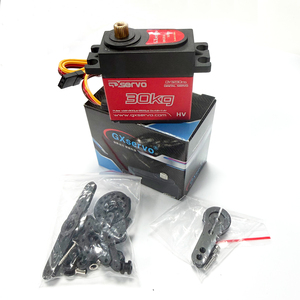
GXservo 30KG High Torque Waterproof Digital Servo
Heavy-duty IP67 waterproof metal gear motor. Built for rugged field robotics, unmanned ground vehicles (UGVs), and demanding duty profiles.
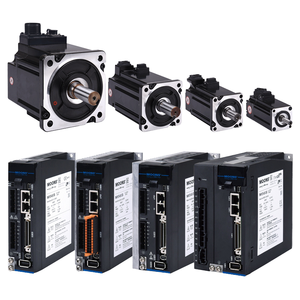
750W 220VAC Servo Motor with Integrated Controller Drive
2.4N.m rated torque system complete with 3m shielded cabling and digital drive. Delivers smooth velocity profiling for industrial automation.
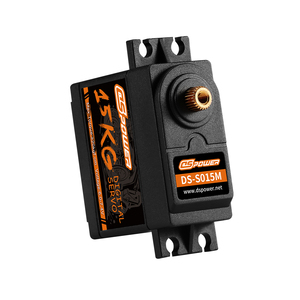
High-Speed Robot Motor with Closed-Loop Feedback (15kg)
High torque density unit equipped with integrated magnetic encoder feedback for exact angular control in automated logistics and cobots.
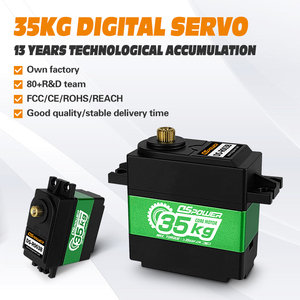
35KG Universal Micro Servo Motor with Metal Gearing
Full aluminum case construction with high thermal dissipation. Engineered for precise high-load steering and robotic arm articulation.
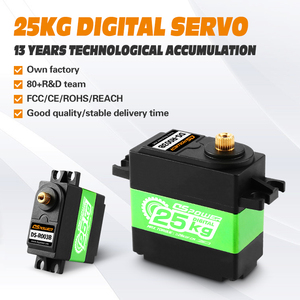
25kg Semi-Aluminum Metal Gear PWM Servo Motor
Optimized power-to-weight ratio. Provides high holding torque and low backlash for robotic joints, RC mechanisms, and automated valves.
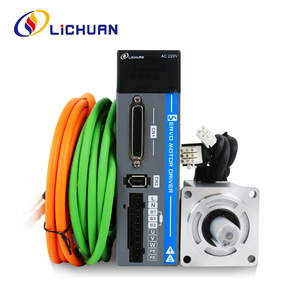
Lichuan IP65 AC Servo Motor & Driver Kit (200W-1000W)
3000RPM industrial-grade servo kit. High ingress protection (IP65) rated for harsh production environments, industrial CNC, and robotics.
Evaluating China's Best Hub Motor Factories: Technical Benchmark & Auditing Framework
Selecting an OEM supplier among China best hub motor factories requires evaluating far more than initial catalog unit price. Direct-drive hub motors (in-wheel BLDC motors) integrate electromagnetic, mechanical, and thermal systems into a tightly constrained envelope—often exposed to severe shock, water submersion, and ambient thermal spikes.
Global original equipment manufacturers (OEMs) across micro-mobility, medical robotics, automated guided vehicles (AGVs), and light electric vehicles (LEVs) rely on Chinese manufacturing hubs in Zhejiang (Ningbo, Taizhou), Jiangsu (Changzhou, Wuxi), and Guangdong (Shenzhen, Dongguan). However, the technical gap between Tier-1 automotive-grade suppliers and low-tier assembly shops is vast. An E-E-A-T (Experience, Expertise, Authoritativeness, Trustworthiness) procurement strategy demands a rigorous technical teardown of supplier capabilities.
Electromagnetic & Lamination Steel Quality
Leading factories utilize ultra-thin 0.2mm to 0.35mm silicon steel laminations (such as Baosteel 20AV1300) to minimize eddy current losses at elevated electrical frequencies. High fill-factor segmented stators with automated needle winding maximize slot fill up to 60%, delivering peak torque density (Nm/kg) without thermal saturation.
Neodymium Magnet Grade & Thermal Stability
Top hub motor manufacturers specify rare-earth NdFeB permanent magnets featuring high Curie temperatures—specifically H, SH, or UH grade magnets (e.g., 38SH or 42UH) rated for continuous operation at 150°C to 180°C. Dysprosium (Dy) and Terbium (Tb) grain boundary diffusion prevents irreversible demagnetization under peak current surge.
Ingress Protection & Dynamic Mechanical Sealing
Because hub motors serve as structural wheel hubs, dynamic shaft sealing is critical. Premium factories employ dual-lip fluoroelastomer (FKM) radial oil seals combined with IP67 or IP68 labyrinth structures and hydrophobic breathable membranes (Gore-Tex vents) to equalize internal air expansion without drawing moisture into the stator chamber.
Key Product Development & Engineering Trends in Hub Motor Systems
The global electric powertrain landscape is transitioning rapidly from traditional central-drive motors coupled with heavy reduction gearboxes toward decentralized, high-efficiency direct-drive and planetary geared in-wheel hub architectures. Procurement teams must align with factories investing in the following forward-looking technologies:
1. Axial Flux vs. Radial Flux Hub Topologies
While radial flux BLDC motors remain the industry standard due to cost-effective automated winding, Axial Flux Permanent Magnet (AFPM) hub motors are gaining rapid traction in high-performance applications. Axial flux designs offer up to 30% higher torque density and a significantly shorter axial length profile. Chinese tier-1 factories are mastering double-rotor single-stator axial flux topologies, allowing compact integration directly within standard wheel rim dropouts.
2. Advanced Thermal Management: Oil-Submerged & Phase-Change Cooling
Thermal dissipation is the ultimate bottleneck for direct-drive hub motors. Without air draft inside an enclosed wheel casing, prolonged steep hill climbing or heavy payload transport can trigger thermal throttling. Advanced China hub motor factories are implementing internal oil-cooling (using dielectric transformer fluids) and phase-change material (PCM) liners that absorb transient peak heat, reducing continuous operating temperatures by up to 25°C.
3. Integration of Silicon Carbide (SiC) In-Hub Drives
The convergence of motor and drive electronics has given rise to Smart Hub Assemblies. By mounting miniaturized, vibration-isolated Field-Oriented Control (FOC) drivers utilizing Silicon Carbide (SiC) or Gallium Nitride (GaN) MOSFETs directly on the motor end-plate, OEMs eliminate long high-current phase wires, lowering Electromagnetic Interference (EMI) and boosting power stage efficiency to over 98%.
Technology Comparison: Direct Drive vs. Geared Hub Architectures
| Technical Parameter | Direct Drive (Gearless) Hub Motor | Internal Planetary Geared Hub Motor | Axial Flux Direct Drive Hub |
|---|---|---|---|
| Torque Density (Nm/kg) | Moderate (3.5 - 5.5 Nm/kg) | High (7.0 - 11.0 Nm/kg at wheel) | Ultra-High (12.0 - 18.0 Nm/kg) |
| Acoustic Noise (dB) | Ultra-Quiet (< 42 dB) | Moderate (< 58 dB, helical gears) | Quiet (< 45 dB) |
| Efficiency Profile | Peak 90-93% at High Speed | Peak 86-89% (Mechanical losses) | Peak 94-96% across wide RPM |
| Maintenance & L10 Life | Zero Gear Wear (>30,000 Hours) | Gear Wear replacing at 10k-15k hrs | Zero Gear Wear (>30,000 Hours) |
| Braking Regeneration | Full Regenerative Braking | Requires freewheel lockup clutch | Full Regenerative Braking |
| Target Application | Heavy LEVs, AGVs, Medical Carts | Light e-Bikes, Foldable Scooters | Performance EV, Robotics, UGVs |
Future Sourcing Trends & Supply Chain Risk Management in China
Global supply chain dynamics dictate that procurement executives move beyond basic transactional purchasing toward strategic partnership integration with qualified Chinese manufacturing entities. Key procurement trends shaping 2025–2030 include:
Dual-Source & Regional Hub Strategy
To hedge against geopolitical friction, freight disruptions, and localized lockdowns, leading brands mandate that their primary Chinese hub motor manufacturer maintains complete tooling mirror sets in alternative manufacturing zones or dual-plant facilities across South China and East China.
100% Automated End-of-Line (EOL) Testing
World-class hub motor factories have eliminated manual sampling checks in favor of fully automated robotic EOL test benches. Every manufactured unit undergoes dynamic back-EMF waveform symmetry checks, cogging torque peak measurement, insulation resistance (Hi-Pot test >1500V), and acoustic spectral analysis before packing.
Turnkey Subassembly Integration (Motor + Gearing + Battery)
Sourcing standalone motors introduces integration risk for OEM engineering teams. The dominant procurement trend is sourcing complete motion subassemblies under a single part number. Industry leaders like Telco Intercontinental Corp. integrate custom BLDC hub motors with matched planetary gearboxes, optical or magnetic encoders, custom wiring harnesses, and advanced battery packs (including emerging sodium-ion chemistry modules for low-temperature resilience).
Enterprise Manufacturing Capabilities & Telco Engineering Advantage
Rooted in engineering heritage established in Houston, Texas in 1985, Telco Intercontinental Corp. bridges North American technical oversight and rigorous quality assurance with the high-capacity, cost-efficient manufacturing ecosystem of audited partner factories in China and Asia.
40 Years of OEM Customization
Whether re-winding a stator for non-standard DC bus voltages (12V to 310V), engineering bespoke shaft geometries, or tailoring mounting flanges, our engineering teams eliminate performance trade-offs inherent in off-the-shelf catalog motors.
Strict Medical & Industrial Compliance
Supporting high-reliability sectors including medical lab automation, infusion devices, and industrial motion control. We adhere strictly to ISO 9001 and ISO 13485 supplier standards with full lot traceability, cleanroom-compatible lubricants, and documented revision control.
Agile Prototype to Mass Production
Modified standard platforms reach first sample validation in as quick as 4 to 6 weeks. Ground-up bespoke motor programs complete Finite Element Analysis (FEA) electromagnetic modeling and DFM sign-off to full production samples within 10 to 14 weeks.
Need a Tailored Hub Motor or Servo Solution for Your Program?
Our US and global application engineers analyze your exact torque-speed profile, continuous duty requirements, thermal boundary conditions, and target BOM cost.
Frequently Asked Questions (FAQ) for OEM Hub Motor Sourcing
Expert answers to common engineering, quality control, and supply chain queries encountered when sourcing hub motors from China factories.
Q1 How do I verify if a China hub motor factory uses real N38SH or higher temperature magnets?
Authenticity verification requires asking for raw material Mill Test Certificates (MTC) and conducting destructive thermal testing. Legitimate suppliers perform BH curve tracer analysis (hysteresisgraph test) at ambient and elevated temperatures (150°C - 180°C). In-house testing involves subjecting sample motors to full continuous torque loads while monitoring thermal demagnetization via back-EMF constants (Ke) before and after heating cycles.
Q2 What are the typical Minimum Order Quantities (MOQs) for custom hub motor development?
For modified standard platforms (shaft, connector, voltage winding adjustments), typical annual MOQs range from 250 to 500 units. For clean-sheet custom programs requiring dedicated die-cast wheel molds, stamped lamination tooling, and custom stator jigs, MOQs usually start at 1,000 units annually. Prototype pilot production runs (5 to 20 units) are supported during engineering validation prior to final tooling sign-off.
Q3 How is cogging torque minimized in high-torque direct-drive hub motors?
Top-tier factories mitigate cogging torque through advanced electromagnetic design: selecting optimal slot-pole combinations (e.g., 12-slot/14-pole, 24-slot/28-pole), implementing skewed stator laminations or skewed magnet arrangements, shaping magnet arc profiles (bread-loaf magnets), and using precise closed-loop FOC drive algorithms with cogging compensation lookup tables.
Q4 What key engineering parameters must be supplied to receive an precise RFQ proposal?
To receive a fully sized motion recommendation, supply: (1) Operating Voltage (VDC/VAC), (2) Continuous & Peak Torque (Nm), (3) Rated & Maximum RPM, (4) Mechanical Envelope/Wheel Diameter, (5) Duty Cycle Profile (On/Off duration), (6) Ambient Operating Temperature & IP Rating requirements, (7) Feedback preference (Hall Sensors, Encoder, Sensorless), and (8) Target Annual Production Volume.
Q5 How do Chinese factories handle IP67 dynamic water and dust ingress protection?
Achieving true IP67 dynamic sealing involves installing dual-lip viton shaft seals, liquid gasket sealant (e.g., Loctite 5699) along hub casing mating seams, O-ring seal grooving on side covers, waterproof cable glands over-molded with epoxy, and 100% automated vacuum leak decay testing on the production line before final assembly.
Q6 Can Telco supply complete subassemblies including matched gearboxes, drives, and batteries?
Yes. Telco specializes in engineered subassemblies. Instead of sourcing motors, planetary gearheads, magnetic encoders, motion controllers, and battery packs (lithium or sodium-ion) from separate vendors, Telco delivers fully validated, integrated motion-and-power subassemblies under a single part number to streamline your BOM and manufacturing line.
Accelerate Your Motion Program with Factory-Direct Engineering
Whether you are designing a next-generation medical device, an autonomous AGV fleet, or high-performance e-mobility products, our engineering team provides rapid dynamic sizing, FEA validation, and transparent factory cost-breakdowns.