Standard & Custom Linear Motion Assemblies
Explore our specialized range of high-precision ball bearing linear guides, micro-linear rails, heavy-duty ball screw modules, and customized OEM sliding units manufactured to ISO 9001 and ISO 13485 standards.
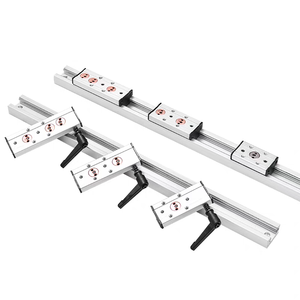
Professional Grade Dual Axis Linear Guideway Rail SGR10/15N/20/25/35
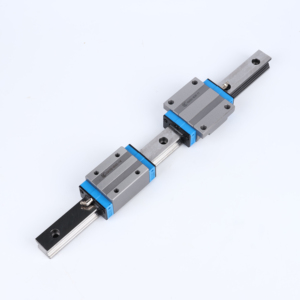
SSAC15CC HGW15 Flange Linear Guide Block & Low Profile Rail
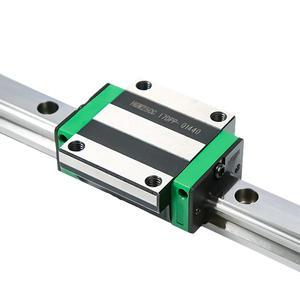
HG Series High-Rigidity Precision Linear Guides (15mm to 65mm)
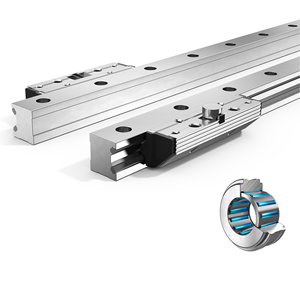
FDA Cleanroom Grade Corrosion-Resistant Linear Guide Assembly
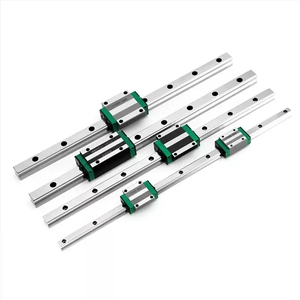
Micro MGN12H / MGN15H Miniature Linear Guide Rail & Block
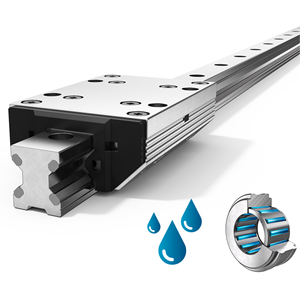
FDC Series Steel Linear Motion Assemblies for Multi-Axis Systems
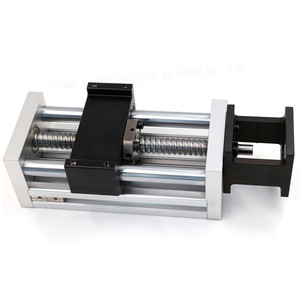
Heavy Duty Ball Screw Driven Linear Stage Module (200mm+ Stroke)
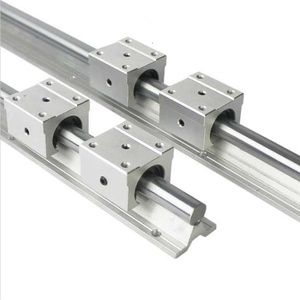
OEM SBR25LUU 25mm Aluminum Linear Rail & Sliding Bearing Unit
Engineering Fundamentals of Precision OEM Linear Motion Technology
A deep analysis of dynamic tribology, load-capacity matrices, surface metallurgy, and kinematic life expectancy for custom linear guide integration.
Kinematic Load Calculations & L10h Nominal Life
Designing modern high-duty automated machinery requires a rigorous calculation of nominal life under combined moment and radial forces. The operational life span ($L$) of a recirculating ball linear guide assembly is expressed via the fundamental Hertzian contact formula:
Where C is the Basic Dynamic Load Rating (N), and P represents the Equivalent Dynamic Load calculated through dynamic loading vectors ($F_{radial}, F_{reverse-radial}, F_{lateral}$).
For custom OEM programs, internal recirculating ball tracks are optimized using a 45° contact angle Gothic arch groove design. This ensures equal load-carrying capacity in the radial, reverse-radial, and lateral directions—providing total mechanical stability regardless of mounting orientation (vertical, horizontal, or inverted ceiling mounting).
Preload Selection & Deflection Dynamics
Preload control is critical to eliminating micro-backlash, elevating systemic rigidity, and attenuating structural vibrations in high-speed CNC milling and precision medical lab equipment. We manufacture custom rail-and-block sets across four standard preload categories:
- ZF (Clearance/Zero Preload): Ideal for smooth manual motion, gravity-fed slides, and low-friction linear transfer.
- Z0 (Light Preload - 0 to 0.02C): Standard for precision optical scanners, 3D printers, and automated pick-and-place arms.
- Z1 (Medium Preload - 0.03C to 0.05C): Required for high-rigidity CNC machining centers, heavy payload industrial robots, and Z-axis stages.
- Z2 (Heavy Preload - 0.06C to 0.08C): Engineered for extreme vibration environments and high dynamic shock loading applications.
Advanced Metallurgy & Anti-Corrosion Surface Treatments
Environmental exposure dictates the lifespan of linear guide components. Standard bearing carbon steel (SUJ2 / GCr15) rapidly degrades when subjected to corrosive fluids, cleanroom washdowns, or moisture. Our custom OEM factory provides specialized metallic surface treatments designed to extend component life by up to 400% in harsh industrial environments.
| Surface Treatment / Material | Hardness (HV) | Layer Thickness | Salt Spray Resistance (ASTM B117) | Primary Industrial Applications |
|---|---|---|---|---|
| Standard Bearing Steel (SUJ2) | HRC 58 - 62 | N/A | 24 Hours | General Industrial Automation, Standard CNC Machinery |
| Raydent Black Oxide Plating | HV 800+ | 2 - 3 µm | 500+ Hours | Semiconductor Equipment, Optical Systems, Cleanrooms |
| Hard Chrome Plating | HV 850 - 1000 | 5 - 10 µm | 100 - 200 Hours | Woodworking Machinery, Outdoor Linear Modules |
| Martensitic Stainless Steel (SUS440C) | HRC 58 - 60 | Integral | 300+ Hours | Medical Diagnostic Analyzers, FDA Food Handling Equipment |
| Armoloy Thin Dense Chrome (TDC) | HV 1100 (HRC 72) | 1 - 4 µm | 1000+ Hours | Marine Engineering, Severe Chemical Exposure & Vacuum Labs |
Key Industry Trends Reshaping Linear Motion Sourcing
How global original equipment manufacturers (OEMs) are updating their mechanical bill of materials (BOM), supply chains, and design standards to maintain a competitive advantage.
1. Shift Towards Fully Integrated Smart Modules
Procurement teams are moving away from sourcing standalone rails, carriage blocks, ball screws, and stepper motors independently. The market is shifting toward pre-aligned, fully integrated single-axis and multi-axis linear actuator stages. This transition reduces machine assembly labor, streamlines supplier management to a single BOM part number, and eliminates mounting stack-up tolerances.
2. Dual-Sourcing & Geographically Resilient Manufacturing
Global supply chain volatility has made single-region procurement a operational risk. Leading OEM brands now demand dual-source manufacturing strategies. By maintaining engineering management in North America alongside primary production lines across specialized hubs in Asia, factories offer OEM buyers guaranteed lead times, safety buffer stock programs, and insulation from geopolitical logistics disruptions.
3. Zero-Maintenance & Self-Lubricating Carriages
Total cost of ownership (TCO) has become a primary selling point for automated machine builders. Modern linear carriage blocks incorporate embedded synthetic oil-impregnated resin reservoirs (E2 self-lubrication modules). These reservoirs continuously deposit an ultra-thin film of oil over the ball bearings during circulation, extending re-lubrication maintenance intervals from 100 km to over 10,000 km of travel distance.
4. Miniaturization for Medical & Semiconductor Equipment
As microfluidics, lab automation, sample handlers, and semiconductor inspection tools shrink in footprint, demand for micro-linear guideways (MGN / MGW series down to 3mm, 5mm, and 7mm rail widths) has expanded. Manufacturing micro-rails requires specialized grinding techniques to maintain sub-micron pitch accuracy without thermal warping.
Why Leading Global OEMs Partner With Our Factory
Building upon four decades of precision motion control heritage, engineering rigor, and strict quality control protocols.
Application Engineering
Our motion engineers analyze your exact dynamic dynamic torque, payload, moment load, and duty cycles before quoting, ensuring optimal system sizing without over-engineering.
Custom Tooling & Sizing
Custom mounting hole pitches, non-standard rail lengths up to 6 meters, special tap sizes, and application-specific carriage wiper seals engineered to your exact CAD specs.
100% Quality Assurance
Every single linear rail and carriage undergoes 3D Coordinate Measuring Machine (CMM) inspection, micro-hardness testing, and laser interferometer parallelism checks prior to packing.
VMI & Kanban Stocking
We reduce your lead times to zero through Vendor-Managed Inventory (VMI), blanket purchase agreements, and safety buffer warehouse stocking in regional hubs.
Frequently Asked OEM Sourcing & Engineering Questions
Answers to common questions regarding tolerances, custom modifications, interchangeability, and minimum order requirements.
Are your custom linear guides interchangeable with major industry brands (e.g., HIWIN, THK, NSK, IKO)?
Yes. Our custom OEM linear rail and block assemblies are designed according to international standard DIN 645 dimensions. Our HG, EG, MGN, and HGW series feature identical mounting hole patterns, assembly heights, rail widths, and carriage dimensions to major brands like HIWIN (HGW/HGH), THK (HSR/SR), IKO, and NSK. You can swap individual carriage blocks or complete rail assemblies without altering your machine chassis CAD drawings.
What is the typical lead time and Minimum Order Quantity (MOQ) for custom OEM orders?
For modified standard linear rails (custom cut-to-length, custom tap holes, special end-step machining), prototype samples are typically delivered in 2 to 3 weeks. Ground-up custom profiles or specialized surface treatments take 4 to 6 weeks. Standard MOQ for modified platforms starts as low as 10 to 50 sets for qualification programs, while full custom OEM programs are scoped at 200+ sets per year.
How do you guarantee parallelism and precision accuracy grades across long rail lengths?
We manufacture linear guide rails across 5 precision grades: Normal (N), High (H), Precision (P), Super Precision (SP), and Ultra Precision (UP). For long rail runs exceeding 4 meters, precision butt-jointing is performed using match-ground rail ends numbered in sequential order. Parallelism of running surfaces is verified using high-resolution Renishaw laser interferometers to achieve running accuracy within 0.003mm per 1,000mm length.
Which lubrication types and seal options are recommended for high-dust or washdown environments?
For dusty environments like woodworking, stone cutting, or agricultural automation, we specify double-lip end seals, bottom seals, inner seals, and metal scrapers that prevent debris ingress. For food-grade and medical applications, we supply FDA-compliant NSF H1 lubricants combined with stainless steel (SUS304/SUS440C) components or Armoloy Raydent surface plating to eliminate flaking or contamination.
What engineering documentation and quality reports do you provide with OEM shipments?
Every OEM production batch includes a comprehensive quality compliance documentation packet: Material Test Certificates (MTC) verifying raw steel heat numbers, Heat Treatment Hardness Depth Reports, 3D CMM Dimensional Inspection Sheets, Salt Spray Testing Logs (for plated rails), and Certificate of Conformance (CoC) matching ISO 9001 and ISO 13485 audit standards.
Partner with a World-Class OEM Linear Guide Manufacturer
Whether you require a custom modified miniature rail, a high-load flange carriage block, or a complete sub-assembled multi-axis ball screw linear stage, our engineering team is ready to review your CAD files and duty cycle profile.
Get a Quote