Featured Precision Motion & Servo Motor Platforms
Directly vetted from top trusted frameless motor factories and motion component foundries. Engineered for high power density, zero-backlash integration, and harsh-environment operating cycles.
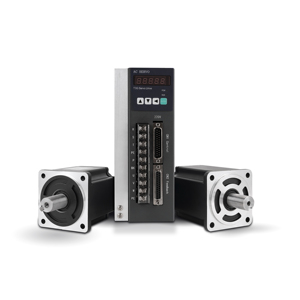
AC Servo Motor 1300W 220V Support Pulse / RS485 Control
Designed for high-precision medical devices requiring continuous positional feedback, minimal electromagnetic interference, and ultra-high dynamic response.
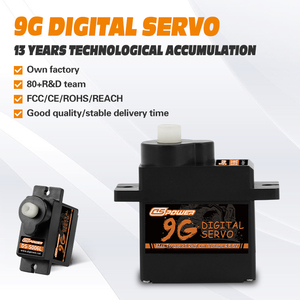
SG90 Servo Motor PWM 180° Micro Servo Motor Series
Ultra-compact 9g actuation platform for lightweight micro-robotics, automated valving, and secondary auxiliary displacement mechanisms.
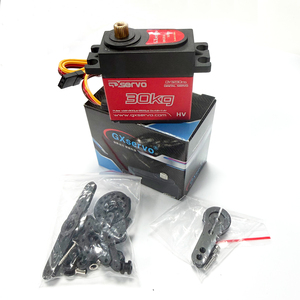
GXservo 30KG High-Torque Waterproof Digital Servo
Heavy-duty IP67-rated housing with full titanium-alloy gear trains designed for rugged field robotics, unmanned surface vehicles, and harsh environments.
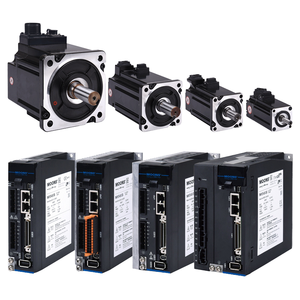
750W 220VAC Integrated Servo Motor with XP Controller
Industrial-grade matched package delivering 2.4 N.m rated torque with 3m shielded cabling, fully compliant with automated assembly lines.
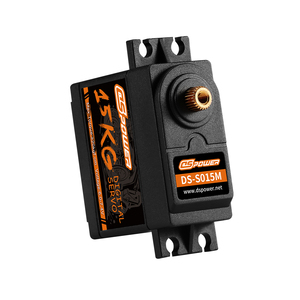
High-Speed RC Robot Motor with Closed-Loop Feedback
15kg-cm torque capacity featuring absolute encoder position feedback, tailored for rapid-indexing robotic arms and pick-and-place automation.
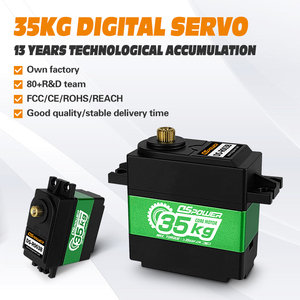
35KG Universal Micro Servo Motor Metal Gear Series
High-density steel gearing within a thermal-dissipating core for high torsional loads, automated steering geometry, and structural joints.
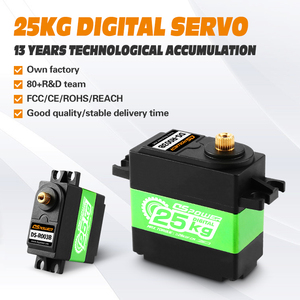
25KG Semi-Aluminum Case PWM Micro Servo
Hybrid aluminum casing optimizing thermal conduction during continuous PWM signal duty cycles in robotic articulation systems.
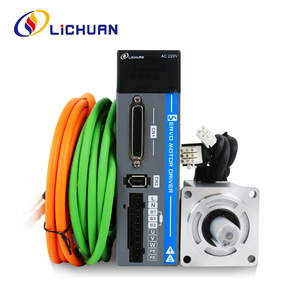
IP65 220V 3000RPM AC Servo Motor & Driver Kit
Complete A5 Series kit scalable from 200W to 1000W, offering IP65 ingress protection for heavy CNC, robotics, and industrial automation.
1. Technical Architecture & Fundamentals of Frameless BLDC Motors
Frameless Brushless DC (BLDC) motors represent the pinnacle of direct-drive electromechanical engineering. Unlike housed traditional motors—which bundle a rotor, stator, bearings, shaft, and enclosure into a pre-sealed unit—a frameless motor is supplied exclusively as two decoupled components: an inner permanent magnet rotor kit and an outer laminated electromagnetic stator core. This minimalist structural paradigm empowers Original Equipment Manufacturers (OEMs) to embed motion generation directly into the structural frame of their machinery, eliminating mechanical compliance, backlash, elastic deformation, and redundant bearing sets.
From a kinematic perspective, integrating frameless motor components directly into driven mechanisms (such as robotic harmonic gearboxes, gimbal axes, surgical arm joints, or semiconductor wafer handlers) vastly optimizes the system's power-to-weight ratio and dynamic responsiveness. By transferring rotational force directly across an air gap into the host structure, engineers eliminate coupling elements—such as flexible shaft couplings, timing belts, and keyways—which are historically responsible for torsional hysteresis, windup errors, and operational friction losses.
Information Gain Insight: Selecting frameless BLDC platforms over traditional housed servos yields up to a 45% reduction in total axial envelope length, doubles dynamic bandwidth, and enhances system stiffness by up to 300% through the elimination of intermediate mechanical coupling compliant nodes.
Electromagnetic Topology: Stator Lamination & Winding Architecture
The performance metrics of a frameless motor factory's output depend heavily on the quality of magnetic steel laminations and copper slot-fill algorithms. High-efficiency frameless stators utilize ultra-thin silicon steel laminations (typically 0.1mm to 0.35mm thickness) insulated by inorganic micro-coatings. Thin laminations reduce eddy current losses during high-frequency electrical commutation, enabling rotational speeds exceeding 20,000 RPM without extreme iron loss heat generation.
Furthermore, leading manufacturing foundries leverage automated precision winding techniques—specifically concentrated fractional-slot concentrated windings (FSCW)—to achieve copper slot-fill factors approaching 65% to 70%. Higher copper fill decreases phase resistance ($R_p$), minimizes thermal dissipation ($I^2R$ losses), and elevates the motor's torque density constant ($K_t$) per unit volume.
| Architecture Parameter | Frameless Motor (Direct Drive) | Housed Brushless Motor | Brushed DC Servo Motor |
|---|---|---|---|
| Mechanical Backlash | 0.0 Arc-Min (Direct Coupling) | 1.0 - 5.0 Arc-Min (Coupling Dependent) | > 8.0 Arc-Min (Gearbox Hysteresis) |
| Torque Density (Nm/kg) | High (7.5 - 14.0 Nm/kg) | Moderate (3.5 - 6.0 Nm/kg) | Low (1.2 - 2.5 Nm/kg) |
| Thermal Dissipation Path | Direct to Machine Chassis (Conduction) | Radiant & Convective via Housing | Internal Rotor Thermal Trapping |
| Bearing Maintenance Interval | Governed by Host Structure Bearings | 10,000 - 20,000 Hours (Factory Locked) | Brush & Bearing Replacement Needed |
| System Compliance (Stiffness) | Ultra-High (> 100,000 Nm/rad) | Moderate (Spring Elasticity in Shaft) | Low (High Hysteresis) |
2. Global Sourcing Trends & Sourcing Matrix for OEM Procurement
As industrial automation shifts toward cobots, autonomous mobile robots (AMRs), drone propulsion, and surgical exoskeletons, procurement managers face growing complexity when evaluating frameless motor factories. Sourcing decisions cannot rest solely on unit purchasing cost; they must incorporate long-term reliability risk, supply chain resilience, magnetic material sourcing continuity, and engineering support capability.
Key Macro Trends Shaping the Motor Supply Chain (2025–2030)
1. Rare Earth Magnet Stabilization & Heavy Rare Earth Minimization: Supply chain exposure regarding Neodymium-Iron-Boron (NdFeB) magnets has catalyzed advanced rotor research. Modern trusted frameless motor factories utilize specialized Dysprosium (Dy) and Terbium (Tb) grain boundary diffusion (GBD) techniques. GBD concentrates heavy rare-earth elements specifically along magnetic grain borders rather than throughout the entire magnet mass, lowering raw material supply volatility while preserving thermal demagnetization immunity up to 180°C.
2. Integration of Advanced Power Electronics & Micro-Drives: Modern OEM engineering favors placing servo drive electronics within millimeters of the frameless stator. This proximity eliminates long motor lead cables, which act as antennas for pulse-width modulation (PWM) electromagnetic interference (EMI). Frameless factories are increasingly supplying pre-tuned electromagnetic rotor/stator kits matched with high-frequency Silicon Carbide (SiC) and Gallium Nitride (GaN) power stages.
3. Transition to Next-Gen Auxiliary Power Integration: Mobile automation platforms increasingly integrate frameless traction and steering motors directly with custom sodium-ion and high-C-rate lithium battery packs. Sodium-ion battery chemistry delivers exceptional low-temperature discharge profiles, enhanced thermal stability, and reduced raw material costs compared to traditional Lithium Nickel Manganese Cobalt (NMC) chemistries, making it an ideal candidate for industrial AMRs operating in cold-chain logistics.
3. Enterprise Manufacturing Audit & Engineering Quality Controls
Evaluating an overseas or domestic frameless motor factory requires strict adherence to international quality standards. Because frameless motor components are shipped exposed—without outer housings to shield stators or lock permanent magnets in place—manufacturing quality protocols must prevent contamination, insulation breakdown, and structural magnet delamination during transport and assembly.
Precision Stator Vacuum Impregnation
Stator coils undergo Vacuum Pressure Impregnation (VPI) using high-grade Class H or Class S epoxy resins. VPI eliminates microscopic air voids within winding slots, dramatically elevating thermal conductivity and dielectric breakdown resistance under high voltage transients.
Automated Rotor Balancing & Sleeving
Permanent magnets bonded to the rotor hub must withstand high centrifugal forces. World-class factories utilize carbon-fiber wrapping or precision non-magnetic stainless steel retention sleeves, coupled with dynamic two-plane balancing to ISO 1940 Grade G1.0.
Back-EMF & Harmonic Waveform Calibration
To deliver smooth torque output free of low-speed ripple, stators undergo automated 100% Back-EMF testing. Pure sinusoidal Back-EMF profiles ensure seamless vector control via Field-Oriented Control (FOC) algorithms.
4. Advanced Engineering Guidelines: Thermal Dissipation & Air Gap Tolerances
Successfully integrating a frameless motor kit into an OEM housing requires diligent attention to thermal expansion co-efficients and radial air gap tolerances. Unlike off-the-shelf housed motors, the machine frame becomes the primary heat sink for the motor's copper losses.
Thermal Path Optimization
During high continuous torque operations, heat generated in the stator windings must conduct outwards through the stator back-iron into the host chassis. OEM design teams must calculate the thermal resistance interface ($R_{th}$) between the stator's outer diameter and the internal bore of the machine housing.
- Interference Fit Pressing: A controlled thermal expansion press-fit (heating the aluminum housing while chilling the stator kit) provides the lowest thermal resistance path, ensuring zero microscopic air gaps.
- Thermally Conductive Structural Epoxies: Where press-fitting is impractical, aerospace-grade conductive potting compounds with thermal conductivity rates exceeding $1.5 \text{ W/m}\cdot\text{K}$ should be specified.
Air Gap Maintenance & Concentricity Tolerances
The mechanical air gap between the outer magnetic face of the rotor and the inner tooth tips of the stator typically ranges between 0.25mm and 0.75mm depending on motor frame size. If machine bearings exhibit structural deflection or machining eccentricities exceed strict limits, un-balanced magnetic pull (UMP) will occur. UMP exponentially increases radial load on system bearings, creating noise, vibration, and premature bearing fatigue.
Enterprise Capabilities & OEM Sourcing Advantage
Anchored by decades of electromechanical engineering, application sizing, and global logistics support, our partnered manufacturing infrastructure resolves core risks in custom motor procurement.
Dual-Source Supply Chain Resilience
With corporate roots dating back to 1985 in Houston, Texas, our engineering and procurement framework combines dual-source manufacturing networks across Asia and North America. This mitigates single-point regional disruptions, tariff fluctuations, and freight bottlenecks, ensuring stable production buffers for high-volume OEMs.
Medical Device Compliance (ISO 13485 & IEC 60601)
We support regulated medical automation and surgical robotic OEMs with rigorous revision control, full lot traceability, cleanroom-compatible synthetic lubricants, low-EMI motor winding selections, and engineering documentation compliant with stringent healthcare audit criteria.
Complete Integrated Subassemblies
Rather than managing multiple vendor relationships for separate motors, encoders, gearheads, and drive electronics, OEMs receive pre-tested, single-part-number subassemblies. Every kit undergoes complete end-of-line verification prior to dispatch.
Cost-Down Electromagnetic FEA Tuning
Our application engineering teams utilize Finite Element Analysis (FEA) to model magnetic flux density, thermal distribution, and structural stress. By right-sizing wire gauges, laminations, and magnet grades to your exact duty cycle, we reduce BOM costs without sacrificing safety margin.
Frequently Asked Questions by OEM Engineers & Sourcing Teams
Direct technical guidance addressing common qualification hurdles, prototyping lead times, customization thresholds, and compliance requirements.
What is the typical Minimum Order Quantity (MOQ) for custom frameless motor programs?
Modified standard platforms—such as specific stack length adjustments, custom lead wire lengths, thermal sensor additions, or modified winding turns—typically start at 250 to 500 units annually. Fully custom ground-up designs involving bespoke lamination dies, proprietary magnet geometry tooling, or custom mechanical hubs are scoped starting at 1,000 units per year. Prototype pilot runs are fully supported during the qualification phase.
What is the standard lead time from initial engineering review to prototype delivery?
For modified standard motor frames, first engineering prototype samples are routinely delivered within 4 to 6 weeks. Ground-up custom electromagnetic designs requiring new lamination stamping tools, custom magnet tooling, and full 3D FEA thermal optimization generally require 10 to 14 weeks, inclusive of DFM review, preliminary sample testing, and validation reporting.
Which specific technical parameters must an OEM provide to initiate application sizing?
To accelerate engineering review, OEMs should provide a detailed duty cycle profile specifying: Continuous Torque ($T_c$), Peak Torque ($T_p$), Operating Speed Range (RPM), Available DC Bus Voltage ($V_{dc}$), Outer Diameter and Axial Envelope constraints, Target Ambient Temperature, IP Rating requirements, expected operating life in hours or cycles, preferred encoder/feedback interface, and agency compliance goals (such as UL, CE, RoHS, REACH, or IEC 60601).
How do frameless motor factories prevent cogging torque in direct-drive applications?
Cogging torque arises from magnetic interaction between rotor permanent magnets and stator teeth slots. Trusted factories minimize cogging through techniques including stator slot skewing, fractional slot tooth geometry optimization, magnet arc shaping, and Halbach array configurations. These methods can reduce cogging torque to under 0.5% of rated continuous torque, ensuring smooth low-speed rotation in surgical devices and optics.
Can matched battery storage solutions be paired directly with custom motor drives?
Yes. For mobile robotics, autonomous carts, and portable equipment, we supply fully integrated power-and-motion packages combining matched frameless BLDC or servo motors, micro-drives, wiring harnesses, and custom sodium-ion or lithium battery packs. This system-level engineering guarantees compatible voltage ranges, discharge rates, and thermal management under a single unified warranty and BOM part number.
Accelerate Your Precision Motion Program
Connect directly with our senior application engineering team to evaluate duty cycles, review dimensional envelopes, and receive comprehensive factory-direct pricing for your next production build.